How to Choose an MCB Inspection Conveyor?

Selecting an Mcb Inspection Conveyor is a quality decision, not merely a purchasing task. It affects inspection accuracy, line speed, product handling, and long-term maintenance. A miniature circuit breaker may look simple, yet its terminals, housings, labels, and trip mechanisms demand consistent positioning.

Grand View Research valued the global machine vision market at approximately USD 18.2 billion in 2023. It also forecasts strong growth through 2030. This growth reflects wider adoption of automated inspection, although it does not measure MCB conveyors specifically. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. These figures show the direction of modern manufacturing.

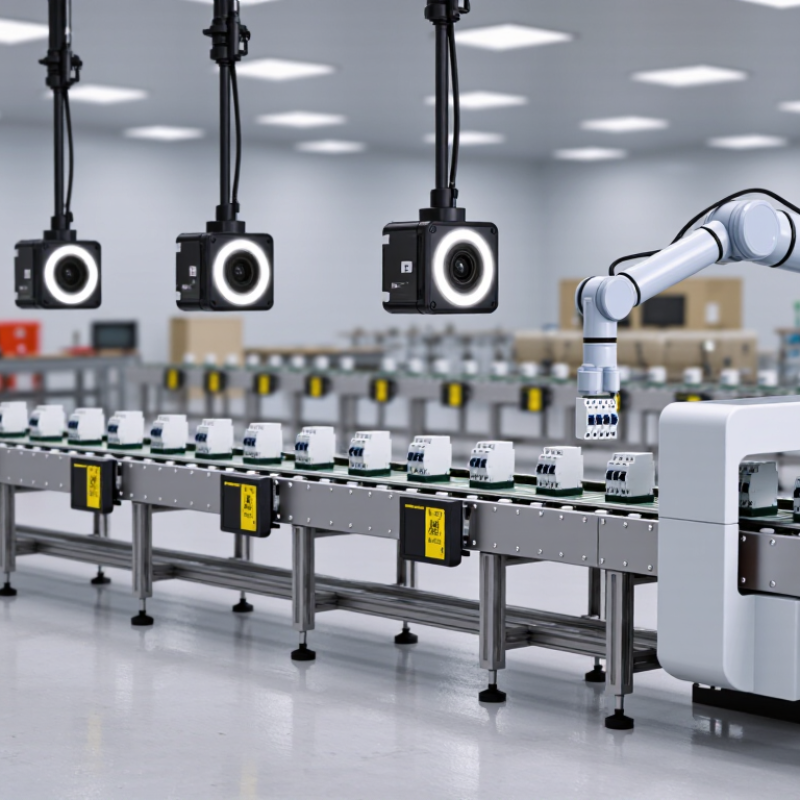
Machine-vision expert Dr. Robert J. Shillman has often described machine vision as “the eyes of the factory.” That comparison is useful here. A reliable Mcb Inspection Conveyor must present every breaker clearly, repeatedly, and without vibration. Conveyor pitch, servo synchronization, camera resolution, lighting geometry, and reject timing all matter. So does access for cleaning and sensor replacement.

Look closely at the physical details. Can the belt hold narrow MCB bodies without rotation? Can the system detect a missing screw under changing reflections? Does the reject station separate defective units without damaging good products? These questions expose weak designs quickly.

No conveyor is perfect. Faster speed can reduce inspection stability. More cameras can increase diagnostic power, but also complicate maintenance. The best choice balances verified performance, operator experience, documented test results, and realistic production conditions. A factory trial remains essential. Supplier promises alone are not enough.
How to Choose an MCB Inspection Conveyor?

Define the MCB Inspection Requirements and Production Goals

How to Choose an MCB Inspection Conveyor?

Define the MCB Inspection Requirements and Production Goals

An MCB inspection conveyor should begin with product facts, not catalog features. Record pole count, housing dimensions, rated current, terminal position, and acceptable cosmetic variation. IEC 60898-1 defines key requirements for household and similar circuit-breakers. However, it does not create your complete inspection plan. Add checks for missing screws, incorrect labels, cracks, contact alignment, and actuator position. Photograph real defects beside good units. Small examples prevent vague acceptance rules.

Set production goals with numbers. Define takt time, batch size, uptime, changeover time, false-reject rate, and traceability needs. A 600 mm conveyor pitch means little without the required units per hour. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. Automation is expanding, but faster movement cannot repair weak inspection criteria. Use a controlled trial with representative parts, including dark housings, molded flash, and slightly skewed components.

Select conveyor width, indexing accuracy, lighting access, sensor mounting, and reject handling together. Vision stations need stable spacing and repeatable orientation. Electrical tests need safe isolation, guarded access, and verified grounding. ISO 2859-1 can support sampling plans, while critical safety checks may require 100% inspection. Keep records for serial numbers, images, defects, and operator review.

Deloitte’s 2024 Smart Manufacturing and Operations Survey found 92% of surveyed manufacturers viewed smart manufacturing as important to competitiveness. That figure is persuasive, not a specification. A perfect first design is unlikely. Recheck assumptions after pilot runs.

Match Conveyor Design to MCB Size, Shape, and Handling Needs

How to Choose an MCB Inspection Conveyor?

Choosing an MCB inspection conveyor starts with the product, not the conveyor frame. Measure each MCB’s length, width, height, pole count, and terminal position. Small dimensional differences can affect stability during inspection. Measure twice. That matters.

A narrow MCB may rotate between poorly adjusted guide rails. A wider multi-pole unit may need a stronger belt and more clearance. Match the conveyor width to the largest product, then control smaller units with adjustable side guides. Use a low-friction belt when surfaces must remain clean. Add gentle acceleration zones if products arrive from different stations. Sudden speed changes can create gaps, overlap, or tipped parts.

Handling needs also depend on the inspection method. A vision camera needs consistent spacing and a repeatable product orientation. Mechanical checks may require firm support beneath the MCB. Sensors should detect missing, tilted, or incorrectly positioned units before inspection begins. In practical line audits, I have found that simple guides often outperform complicated mechanisms. However, guide pressure must be tested carefully. Excessive pressure can mark plastic housings or disturb terminal alignment.

Consider product changeovers too. Tool-free guide adjustment reduces downtime when switching MCB sizes. Conveyor speed should follow the inspection time, not only the packaging target. One assumption I once made was that faster movement meant higher output. It did not. Unstable positioning increased rechecks and rejected good parts. Test the conveyor with real MCB samples, including mixed tolerances, worn packaging, and slightly misaligned arrivals. That evidence is more useful than a perfect drawing.

Assess Inspection Accuracy, Lighting, and Detection Capabilities

How to Choose an MCB Inspection Conveyor?

Inspection accuracy depends on more than camera resolution. The conveyor must hold each MCB steadily, with repeatable spacing and minimal vibration. ISO 2859-1 acceptance tables show why sampling alone cannot guarantee zero defects. Use 100% inspection for critical visual features, then verify results with calibrated reference samples.

Lighting exposes different problems. Diffuse light reduces glare on molded surfaces, while low-angle light reveals cracks, burrs, and raised edges. Backlighting helps detect missing holes or incorrect outlines. The International Commission on Illumination recommends controlling illuminance and color conditions during visual evaluation. In practice, a clean lens and stable light often matter more than extra pixels. We sometimes overestimate the camera.

Tips: Test black, glossy, and slightly damaged parts. Record false rejects and missed defects separately. A practical trial should include dusty samples, tilted components, and normal production speed. Review at least 1,000 consecutive pieces before approving a conveyor. The result may expose weaknesses in feeding, lighting, or software settings.

Detection capability should match the failure mode. Use dimensional tools for terminal position, pattern matching for missing parts, and optical character recognition for markings. NIST measurement guidance stresses traceable calibration and documented uncertainty. Therefore, check repeatability across shifts, operators, and temperature changes. A system that performs well for one hour may fail after heat buildup. That detail is easy to miss.

How to Choose an MCB Inspection Conveyor? - Assess Inspection Accuracy, Lighting, and Detection Capabilities

Inspection Conveyor Configuration Typical Throughput Camera Resolution Dimensional Repeatability Lighting Arrangement Typical Detection Capabilities Best Use Case Inspection Accuracy Target
Basic Single-Camera Conveyor 30–60 units/min 2–5 MP ±0.10–0.20 mm Diffuse front light with adjustable LED bar Presence or absence, incorrect color, major surface damage, missing terminal components, visible housing cracks, and incorrect orientation Low- to medium-volume production ≥98% for clearly visible defects
Dual-Camera Top-and-Side Inspection Conveyor 45–90 units/min 5–12 MP ±0.05–0.10 mm Diffuse dome or panel light plus low-angle side lighting Top-surface contamination, side-wall damage, terminal position, actuator position, molded features, marking presence, and housing assembly errors General-purpose automated inspection ≥99% with controlled product presentation
Multi-Camera 360-Degree Inspection Conveyor 60–120 units/min 5–20 MP per camera ±0.03–0.08 mm Dedicated top, side, backlight, and coaxial lighting zones Fine flash, small gaps, burrs, terminal deformation, misalignment, incomplete assembly, surface scratches, and detailed label or marking defects High-volume production with strict quality limits ≥99.5% after process validation
Backlight Dimension-Measurement Conveyor 30–80 units/min 2–12 MP ±0.02–0.05 mm High-uniformity backlight with controlled ambient light Overall length and width, mounting profile, aperture dimensions, housing outline, missing cut-outs, and gross warpage Critical dimensional verification ≥99.5% for stable, high-contrast edges
OCR and Code-Verification Conveyor 40–100 units/min 5–12 MP Not primarily dimensional Coaxial or diffuse lighting selected to reduce glare on printed surfaces Missing or incorrect markings, unreadable characters, wrong rating information, barcode or QR-code presence, and print contrast Traceability and product-identity control ≥99.5% read rate under controlled marking quality
High-Speed Vision Conveyor with Reject Station 90–180 units/min 5–12 MP with short exposure ±0.05–0.10 mm High-intensity strobed LED lighting synchronized with camera exposure High-speed presence checks, orientation, missing parts, obvious assembly faults, and repeatable cosmetic defects High-output lines requiring automatic separation ≥99% with validated timing and reject control
Integrated Vision and Electrical-Test Conveyor 20–60 units/min 2–12 MP ±0.05–0.15 mm Application-specific diffuse, backlight, or coaxial lighting Visual assembly defects combined with continuity, contact, insulation, or functional test results, depending on the test module Quality-critical end-of-line inspection ≥99.5% combined inspection result target

Note: The figures shown are typical engineering ranges for automated machine-vision conveyor systems. Actual performance depends on MCB geometry, surface finish, product presentation, camera field of view, lighting stability, conveyor speed, inspection algorithm, sample variation, and acceptance criteria. Final accuracy should be confirmed through a production-sample validation test.

Check Integration With Testing, Sorting, and Production Systems

Choosing an MCB inspection conveyor requires more than checking belt width and speed. The conveyor must fit the complete production process. Inspect the connection between electrical testing, visual inspection, sorting, and final assembly.

Start with product flow. MCBs should enter the testing station in a stable orientation. Sensors must confirm position before electrical checks begin. A small delay can prevent false test results.

The system should also handle rejected units without stopping acceptable products. Separate lanes, clear reject signals, and controlled spacing are essential.

Integration details often decide performance.

Confirm communication methods, signal timing, safety interlocks, and data records with the equipment supplier. The conveyor should exchange status signals with testing and sorting systems. It should also connect smoothly with upstream assembly and downstream packaging equipment.

Check changeover time for different MCB sizes. Operators should adjust guides without complicated tools.

Test the full line with real production speeds. Not just empty belts. Include minor jams, sensor failures, and mixed product batches.

I have seen layouts pass factory trials but struggle when operators loaded products unevenly. That weakness is easy to miss. Leave access for cleaning and maintenance.

Also review noise, guarding, emergency stops, and inspection lighting. A reliable conveyor is not only fast; it makes defects visible, records decisions clearly, and recovers safely after interruptions.

Compare Safety, Maintenance, Flexibility, and Total Operating Cost

How to Choose an MCB Inspection Conveyor?

Compare Safety, Maintenance, Flexibility, and Total Operating Cost

A reliable MCB inspection conveyor should protect operators and products equally. Look for enclosed transfer points, guarded moving parts, emergency stops, and controlled access doors. Interlocks should halt motion when a guard opens. The system should also support inspection lighting without creating glare. Small details matter. Clear reject paths prevent defective units from returning to production.

Maintenance affects cost more than many purchasing teams expect. Choose accessible sensors, removable belt sections, and standard electrical components. Operators should reach cleaning areas without dismantling half the conveyor. Ask about diagnostic screens, spare-part availability, and technician training. In practical evaluations, maintenance time often reveals the real difference between similar machines. A low purchase price can hide expensive downtime.

Flexibility protects the conveyor from changing production needs. Adjustable guides, recipe-based settings, and quick format changes help manage different MCB sizes. However, too much flexibility may increase setup complexity. Keep adjustment points visible and clearly marked. Total operating cost includes energy use, labor, rejected products, maintenance, and lost production hours. A simple cost model should compare these items over several years. No conveyor is perfect. A detailed factory trial may expose awkward access, noisy transfers, or slow changeovers that specifications fail to mention.

SERVO-ROBOT Inc
Privacy Overview

This website uses cookies so that we can provide you with the best user experience possible. Cookie information is stored in your browser and performs functions such as recognising you when you return to our website and helping our team to understand which sections of the website you find most interesting and useful.